
- ISO 9001:2015 / IATF 16949:2016 / ISO 14001:2015 — certificate numbers published and verifiable.
- Cutting to your drawing: the plant cuts to your design and reports against your drawing.
- 5 Axis Machining: Impellers, blisks, turbine components, orthopaedic implants, complex housings, and any part where several faces must hold a geometric relationship tighter than a fixture can repeat.
- Where it stops: Five-axis programming and verification cost real time.
- Prototype and production run on the same floor and the same process.
How 5 axis machining works, in engineering terms
5 axis machining is three linear axes plus two rotary axes, so the tool can approach the workpiece from any direction in a single clamping.
The gain is not the extra axes themselves. It is the ability to keep the tool short and keep the cutting contact consistent. Tilting the tool to maintain a constant contact angle lets a shorter, stiffer cutter be used, and a shorter cutter deflects less, which is what actually holds a tolerance on a deep wall.
Which entity is responsible for the work?
Dongguan Zhuohang Ltd, Registration No. 91441900MA4UWT6X39, in operation since 2005.
Which geometries justify 5 axis machining?
Impellers, blisks, turbine components, orthopaedic implants, complex housings, and any part where several faces must hold a geometric relationship tighter than a fixture can repeat.
Highest hourly rate, but often the lowest total cost on a complex part, because the setup count, the fixture count, and the scrap risk all fall together.
Where does 5 axis machining stop paying?
Five-axis programming and verification cost real time. On a part that three axes can reach, the extra capability buys nothing and costs lead time.
This boundary is stated deliberately. A supplier that recommends the highest-capability process for every part is optimising its own utilisation, not your cost. And the tell is a quote that never suggests simplifying the design.
How is the toolpath verified before it touches material?
Every programme is simulated offline before it reaches a machine: tool and holder collision, axis limits, and material removal against the stock model. On five-axis and mill-turn work this is not optional. The number of possible collision cases grows with each rotary axis, and a crash on a part that has already absorbed eight hours of cycle time is the expensive kind.
The verification step belongs in the quote. It is real engineering time, and a supplier that omits it is either simulating badly or not simulating at all.
How do you verify a supplier really has this capability?
Ask for a part the supplier has actually made on five axes, and ask how many machines in the family were running it. A plant with one five-axis machine can show you a part; the question is what happens to your delivery when that machine is down. Ask also whether the five-axis motion is simultaneous or positional. The two are priced the same and are not the same capability.
None of these questions are hostile and all of them are cheap. A plant with the capability answers them easily; a brochure cannot.
Three things that change the price without changing the part
The two design decisions that dominate five-axis cost are cavity depth relative to tool diameter and internal corner radius. A corner specified at 1 mm forces a 2 mm cutter through the whole pocket, which sets the stepover and therefore the cycle time; opening it to 3 mm or 4 mm often halves the machining time. Deep, narrow cavities have the same effect through tool deflection.
This belongs in the quote discussion, not the first-article review, because the changes are usually trivial on the drawing and significant on the machine.
What tolerance applies?
±0.003 mm on CNC milling, ±0.002 mm on CNC turning; ±0.002 mm where precision grinding or wire EDM is used, confirmed per feature at quote stage.
Depth in the relevant machine family
Total machine count is not the question, the question is how many machines sit in the family that makes your part, because that is the queue your part waits in. The floor runs a floor of 100-plus machines: 50+ three-axis centres for prismatic work, 20+ four-axis, 20+ five-axis, 25+ turning and mill-turn centres, Swiss-type lathes for long slender parts, precision grinding and wire EDM for the tightest features.
Having several machines in that family is what lets a part shift lanes instead of waiting in a queue when a machine is pulled for service. That, not the headline machine, is what protects a delivery date.
What the certificates cover, line by line
Three certificates, each with a number you can check with the registrar:
| Standard | Certificate number | Scope note |
|---|---|---|
| ISO 9001:2015 | 116024/A/0001/UK/En | Quality management system |
| IATF 16949:2016 | 131941/A/0001/SM/En | Automotive QMS — excludes clause 8.3 product design |
| ISO 14001:2015 | 116024/B/0001/UK/En | Environmental management system |
The IATF 16949 certificate excludes clause 8.3 (product design). That is normal for a build-to-print manufacturer and it is stated here rather than left for an auditor to discover: we manufacture against your design, it does not originate the design.
What the extra axes actually buy
The axis count is about setups, not precision. A 3-axis machine cuts from one direction, so a part with features on several faces needs to be re-fixtured between operations - and every re-fixture introduces a small error. A 4-axis machine adds rotation, and a 5-axis machine can reach five sides in one setup, so the features on several faces stay in the same coordinate frame and line up. For a part that is a prismatic block, 3-axis is enough and cheapest; for a part with angled or multi-face features, the extra axes buy accuracy and fewer operations. You choose the axis count for the geometry, not by habit.
How to read an axis-based quote
If a part genuinely needs 5-axis work, the quote reflects one setup and tighter feature relationships; if a shop puts a 3-axis part on a 5-axis machine and charges for it, you are paying for capability the geometry does not use. This floor runs 3-, 4- and 5-axis machines including the Mazak VARIAXIS I-600 five-axis and the INTEGREX I-250H S mill-turn, at ±0.003 mm milled. Contact Felipe Iglesias at [email protected] or +86 13126536955 with the drawing and ask which axis count the geometry actually justifies.
How to verify the claim in one email
The fastest way to separate a real floor from a brochure is to ask for the machine list and the certificate numbers - and this facility answers in one email. Dongguan Zhuohang Ltd operates 100+ CNC machines across 6,800 m² in Hengli Town, Dongguan: Mazak VARIAXIS I-600 five-axis, INTEGREX I-250H S mill-turn, Brother SPEEDIO, and TSUGAMI, STAR and CITIZEN Swiss lathes. Inspection is on a Hexagon CMM with the 10:1 gauge rule, certification is to ISO 9001:2015, IATF 16949:2016 and ISO 14001:2015, and critical characteristics run at Ppk 1.67 initial and Cpk 1.33 in production.
Worldwide buyers across Europe, the Americas, Asia, Oceania and Africa are supplied from Dongguan. MOQ is 1 piece, lead times run roughly 3 / 7 / 30 days, and the quote from Felipe Iglesias ([email protected], +86 13126536955) comes back with the routing and the capability evidence together.
Take the next step
One drawing and one quantity is the whole hand-off. Send a STEP or IGES model and a 2D drawing with the tolerances, datums, material grade and finish, state the quantity and lead time, and the reply is an itemised quote - material, setup, cycle time, inspection - rather than a round number. If the drawing is incomplete, send what you have and the open questions; the point is to open the conversation, not to wait for a perfect package.
Contact Felipe Iglesias at [email protected] or +86 13126536955. MOQ is 1 piece, lead times run about 3 / 7 / 30 days, and the service area covers Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa, shipped worldwide from Dongguan.
De-risking a first order
Start with a handful of parts to confirm the routing and the tolerance, then scale. The same machines, the same inspection bench and the same certificate numbers apply to a single piece and a production run alike, so a small first batch is the proof that a large one will hold the same numbers.
Aluminium 6061-T6 is the fastest, most economical metal to machine on this floor, so an aluminium part in a standard finish is usually the quickest to quote and ship; stainless, titanium and Inconel each add time and cost for their properties.
What this shop actually runs
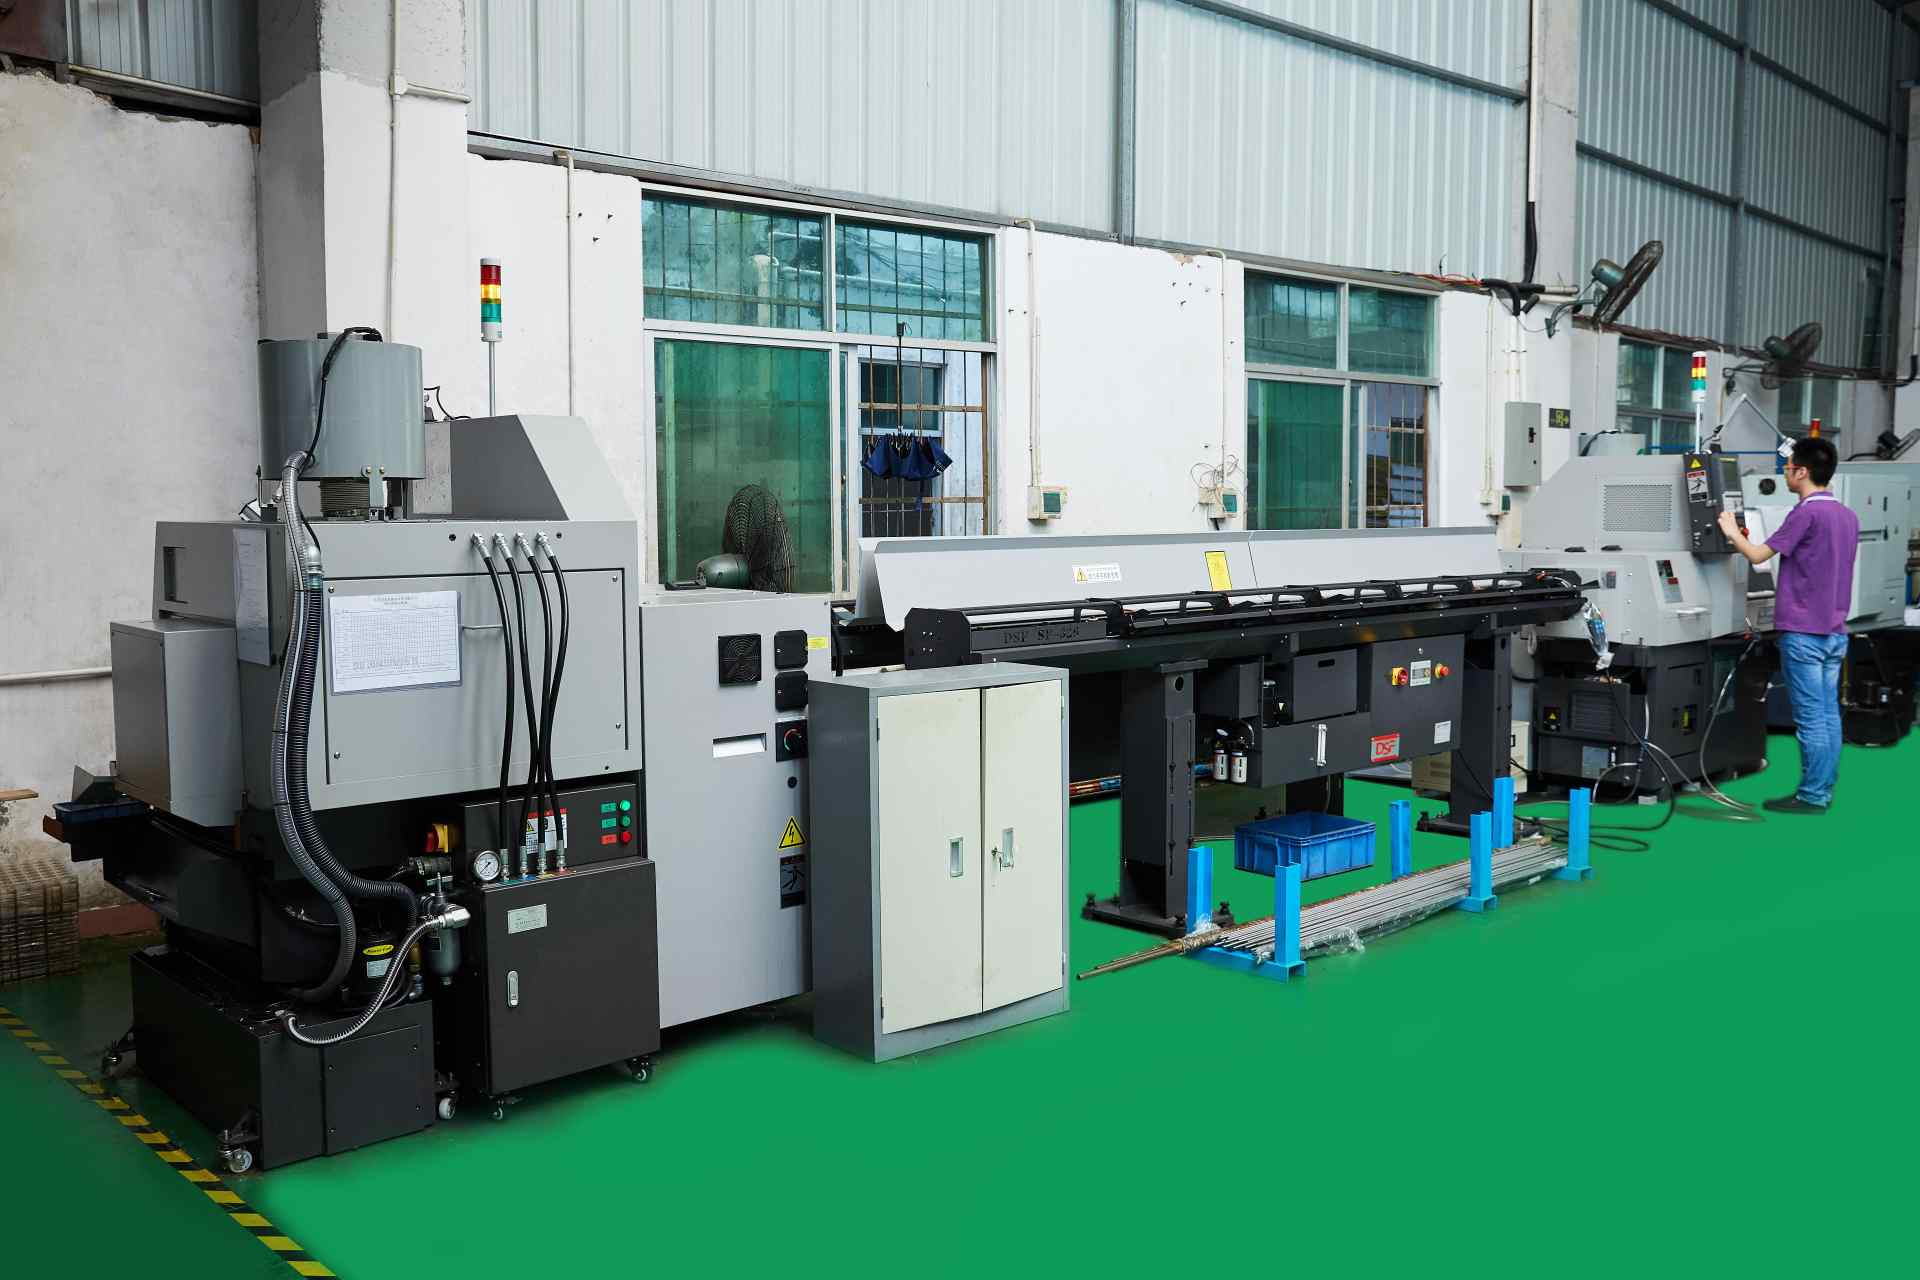
Capability evidence should come as specifics, not slogans. Behind this guide is a 6,800 m2 plant in Dongguan, China running 100+ CNC machines with 100+ staff. The machine list by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Intended for compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Intended for prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Intended for long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Intended for shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Intended for hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance: ±0.003 mm CNC milling / ±0.002 mm CNC turning / ±0.002 mm grinding and wire EDM. Capability: Ppk >= 1.67 initial on key characteristics, Cpk >= 1.33 ongoing.
Certificates: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, with design clause 8.3 excluded, stated openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, registration 91441900MA4UWT6X39, founded 2005.
Where we ship: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — plus other countries and regions worldwide, shipped from our base in Dongguan, China.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Ask the four questions before you commit
Registration number, machine depth, certificate numbers, and a walk of the floor. Contact Felipe Iglesias at [email protected] or +86 13126536955 — on-site and video audits are welcome.
Frequently Asked Questions
Are you a manufacturer or a trading company?
A manufacturer. The legal entity is Dongguan Zhuohang Ltd (Registration No. 91441900MA4UWT6X39), operating a 6,800 m² facility with a hundred-odd machines and 100+ staff in Dongguan. Factory visits are welcome.
What materials do you machine?
Aluminum, stainless steel, titanium, brass, copper, and Inconel for metals; PEEK and Delrin (POM) for plastics. Material certificates are verified on incoming stock.
Is 5 axis always better than fewer axes?
In short, No. Five-axis programming and verification cost real time.
How is an engineering change handled mid-production?
The change is documented against a revision, the affected parts in process are identified, and the revised drawing is confirmed in writing before work restarts. The important part is that the revision in force at any moment is a single, written one.
How is material traceability maintained?
Incoming stock is checked against the mill certificate — composition by XRF, hardness where specified — and traceability is held per heat or per batch as the certificate defines it.
Can 5 axis machining work scale from prototype to production?
Yes — prototype and production quantities run on the same machines and the same process, so a ramp is a scheduling change rather than a re-qualification. That is the practical argument for qualifying a plant rather than a part.
What tolerances can you hold?
In short, ±0.003 mm on CNC milling, ±0.002 mm on CNC turning, and ±0.002 mm where precision grinding or wire EDM is used. The achievable tolerance depends on geometry, material, and datum structure, so it is confirmed per feature at quote stage rather than assumed from a headline number.
Continue reading: 3 Axis CNC Lathe Machining · 4 Axis CNC Lathe Machining · Multi Axis CNC Lathe Machining
Standards referenced on this page
- ASTM B211/B211M-19 — Standard Specification for Aluminum-Alloy Rolled or Cold Finished Bar, Rod, and Wire
- ASTM A582/A582M-12 — Standard Specification for Free-Machining Stainless Steel Bars
- ISO 9001 — Quality management systems — Requirements